Why Is Raw Material Control Key for Orthopedic Implants?
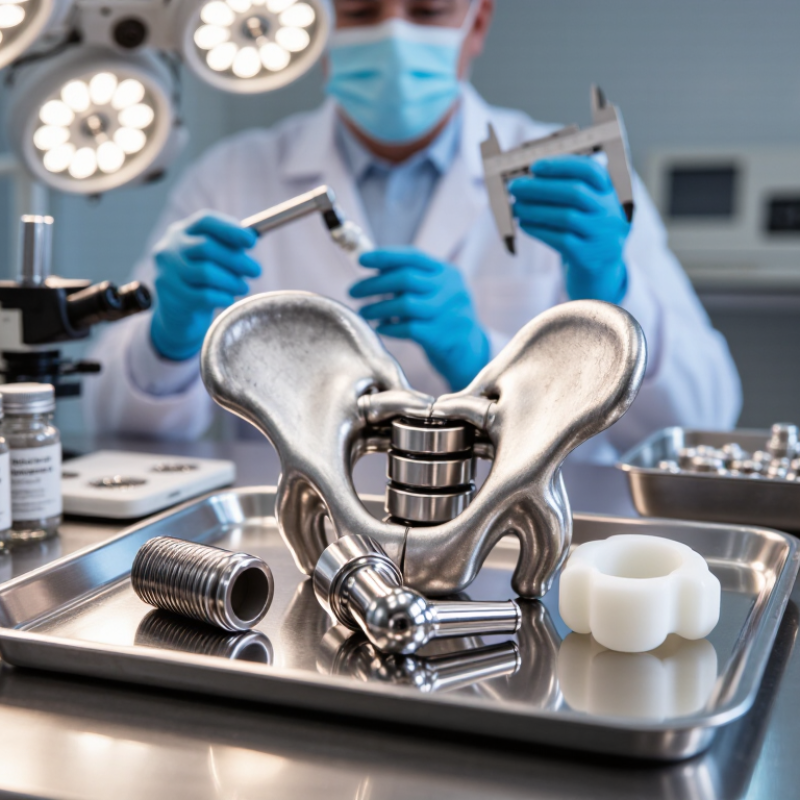
Why is raw material control critical for orthopedic implants? The answer begins with the body’s intolerance for uncertainty. An implant may remain inside a patient for decades. Small changes in titanium purity, cobalt-chromium composition, surface roughness, or polymer cleanliness can affect wear, corrosion, fatigue, and bone attachment.
The U.S. Food and Drug Administration requires manufacturers to characterize materials, control suppliers, and verify production consistency. ASTM standards, including ASTM F67 and ASTM F136, define requirements for commercially pure titanium and titanium alloys used in surgical implants. The 2024 Australian Orthopaedic Association National Joint Replacement Registry also shows why long-term monitoring matters. It tracks more than two million joint replacement procedures and reports revision outcomes across implant designs and materials. These records do not prove that every failure begins with raw materials. Still, they expose how material decisions can influence clinical durability.
W. Edwards Deming, a leading quality-management expert, stated, “Quality comes not from inspection, but from the improvement of the production process.” That principle fits implant manufacturing closely. Incoming inspection alone cannot repair contaminated powder, unstable alloy chemistry, or inconsistent ceramic properties.
Controls must reach the mine, mill, powder supplier, machining line, and sterilization process. Traceability matters. So does humility. Even well-documented systems can miss unexpected interactions between material, design, and patient biology. Effective raw material control therefore combines supplier audits, chemical analysis, mechanical testing, surface inspection, and batch-level records. The objective is not simply compliance. It is predictable performance inside a living body.
Why Is Raw Material Control Key for Orthopedic Implants?
Raw material control defines what enters an orthopedic implant before machining, coating, or sterilization begins. Its scope covers supplier approval, material grades, chemical composition, mechanical properties, surface condition, packaging, and traceability. For titanium, cobalt-chromium alloys, and stainless steel, teams verify elements such as nickel, chromium, oxygen, and carbon against approved specifications. They also review mill certificates and confirm results through independent testing when risk justifies it.
Traceability matters. Each billet, powder lot, or polymer batch should connect to a supplier record, inspection result, and production history. ISO 13485 requires documented controls for purchased products, while ISO 5832 standards define requirements for metallic implant materials. ASTM testing methods add practical checks for tensile strength, fatigue performance, corrosion resistance, and cleanliness. Small deviations matter. A rough surface, hidden inclusion, or incorrect heat treatment can influence wear and long-term fixation.
The National Joint Registry’s 20th Annual Report recorded more than four million hip and knee procedures, showing the scale of evidence behind implant surveillance. Its revision data also reminds manufacturers that performance depends on many variables, not materials alone. Raw material control reduces uncertainty, but it cannot remove it. Supplier audits may miss process drift. Sampling plans may overlook rare defects. That gap deserves review through trend analysis, nonconformance investigations, and periodic requalification. A strong system therefore treats material control as an active engineering process, not a certificate-collection exercise.
| Control Dimension | Definition and Scope | Typical Orthopedic Implant Materials | Key Requirements or Tests | Why It Matters | Typical Objective Evidence |
|---|---|---|---|---|---|
| Material Identity | Verification that the received material is the specified alloy, polymer, ceramic, or composite grade. | Titanium and titanium alloys, cobalt-chromium alloys, stainless steel, ultra-high-molecular-weight polyethylene, ceramics, and bone cement components. | Certificate review, positive material identification, chemical composition testing, and grade confirmation against the approved specification. | Incorrect material identity can change strength, corrosion behavior, wear performance, and biological response. | Approved material specification, supplier certificate, test report, receiving inspection record, and lot traceability. |
| Chemical Composition | Control of alloying elements, impurities, residuals, and restricted substances within defined limits. | Titanium alloys containing aluminum and vanadium; cobalt-chromium alloys containing chromium and molybdenum; austenitic stainless steel; implant-grade polymers. | Elemental analysis, impurity limits, carbon or nitrogen control where applicable, and comparison with recognized material specifications such as ASTM or ISO standards. | Composition affects mechanical properties, passivation, corrosion resistance, processing response, and potential ion release. | Laboratory chemical analysis, supplier test certificate, approved material standard, and nonconformance records. |
| Mechanical Properties | Control of strength, ductility, hardness, elastic modulus, fatigue behavior, and fracture resistance required for the intended anatomy and load. | Titanium alloys for high strength-to-weight performance; cobalt-chromium alloys for wear and strength; stainless steel for selected fixation applications; polymers for bearing surfaces. | Tensile testing, yield strength, elongation, hardness, fatigue testing, and fracture toughness where relevant. | Mechanical variability may contribute to deformation, loosening, fatigue fracture, or loss of fixation. | Material test report, heat-treatment record, batch test results, sampling plan, and acceptance criteria. |
| Microstructure and Thermal History | Control of grain structure, phase balance, inclusions, porosity, and the effects of melting, forging, machining, annealing, or other thermal processes. | Forged titanium and cobalt-chromium alloys, cast or wrought stainless steel, and thermally processed polymers and ceramics. | Metallographic examination, grain-size measurement, phase evaluation, inclusion assessment, porosity inspection, and furnace-cycle review. | Microstructural defects can reduce fatigue life, increase crack susceptibility, and affect corrosion or wear performance. | Microstructure reports, heat-treatment charts, process validation records, and material release documentation. |
| Surface Condition | Control of roughness, oxide condition, cleanliness, residues, surface damage, and coatings before or during manufacturing. | Metallic implant surfaces, porous coatings, ceramic bearing surfaces, and polymer components. | Visual inspection, surface roughness measurement, coating thickness or adhesion testing, particulate evaluation, and residue testing. | Surface condition influences osseointegration, friction, wear, corrosion, coating durability, and cleaning effectiveness. | Inspection records, coating certificates, roughness data, cleaning validation results, and surface acceptance criteria. |
| Biocompatibility-Relevant Characteristics | Assessment of material-related biological risks, including toxicity, sensitization, irritation, systemic effects, and implantation-related responses. | Metals, polymers, ceramics, adhesives, colorants, lubricants, and processing residues that may contact the patient. | Biological evaluation based on the nature and duration of body contact, supported by chemical characterization and applicable ISO 10993 methods. | Material changes or contaminants may introduce biological hazards even when mechanical performance remains acceptable. | Biological evaluation plan, chemical characterization, supplier declarations, extractables data, and risk-management records. |
| Corrosion and Ion Release | Control of electrochemical stability, galvanic interactions, corrosion products, and metal-ion release in the intended physiological environment. | Titanium alloys, cobalt-chromium alloys, stainless steel, and combinations of dissimilar metals. | Corrosion testing, passivation verification, galvanic compatibility assessment, and evaluation of surface defects or contamination. | Corrosion can weaken components and generate products that may cause local tissue reactions or compromise implant performance. | Corrosion test reports, passivation records, material-combination assessment, and surface-process validation. |
| Cleanliness and Contamination | Control of particles, oils, residues, detergents, foreign fibers, and other contaminants introduced during storage, handling, and processing. | All implant materials, especially finished metallic surfaces, porous structures, polymer components, and articulating parts. | Particulate analysis, nonvolatile residue testing, visual inspection, cleaning validation, and controlled packaging. | Contamination can interfere with sterilization, trigger biological reactions, increase wear, or reduce coating and bonding performance. | Cleaning validation report, environmental monitoring records, inspection logs, packaging controls, and deviation reports. |
| Traceability and Lot Control | Ability to link each material lot to its supplier, certificate, inspection results, processing history, finished device, and distribution records. | Raw metals, polymers, ceramics, coatings, additives, packaging-contact materials, and sterilization-related materials. | Unique lot identification, status labeling, documented material receipt, controlled release, and record retention. | Traceability enables targeted investigation, effective containment, and risk-based recall decisions. | Batch records, inventory logs, electronic traceability records, supplier certificates, and release approvals. |
| Supplier and Change Control | Qualification and ongoing monitoring of material suppliers, including review of changes to composition, source, process, site, or test methods. | All critical raw materials and special-process inputs used in implant manufacturing. | Supplier qualification, audits where justified, quality agreements, change notifications, incoming inspection, and requalification. | Unassessed supplier changes may alter material performance without an obvious change in the finished device appearance. | Approved supplier list, audit reports, change-control records, quality agreements, and supplier-performance metrics. |
| Storage and Environmental Control | Control of temperature, humidity, light, packaging integrity, shelf life, and segregation during material storage. | Polymers, bone cement components, adhesives, powders, coatings, and corrosion-sensitive metallic materials. | Defined storage conditions, expiry-date control, container inspection, first-in-first-out or approved stock rotation, and quarantine status control. | Improper storage can cause oxidation, moisture uptake, degradation, contamination, or reduced processing performance. | Temperature and humidity records, inventory status, shelf-life review, packaging inspection, and material disposition records. |
| Applicable Standards and Quality-System Controls | Integration of material requirements into the medical-device quality system, risk-management process, design controls, purchasing controls, and production controls. | Metallic materials described in relevant ASTM or ISO material standards; biological evaluation under applicable ISO 10993 standards; quality systems aligned with ISO 13485 principles. | Approved specifications, risk-based acceptance criteria, validated test methods, nonconformance control, corrective action, and documented release decisions. | A documented system makes raw-material decisions consistent, auditable, and connected to implant safety and performance. | Quality procedures, risk-management files, design-history records, inspection plans, audit findings, and corrective-action records. |
Trace elements and inclusions can reduce corrosion resistance, fatigue strength, and tissue compatibility. A tiny particle may start a crack.
Review melt records, chemical results, heat treatment data, and lot traceability. A certificate alone is not enough.
No. Independent verification can uncover sampling errors, mixed lots, or incomplete records. Purity needs evidence.
Testing may include chemical composition, tensile strength, microstructure, oxygen, nitrogen, inclusions, and corrosion behavior.
Yes. Titanium alloys may need microstructure reviews. Stainless steel needs cleanliness and corrosion checks. Polymers require molecular and contamination data.
Each implant should link to its heat number, inspection results, processing records, and packaging history. A shipment date is not enough.
Audits should review equipment calibration, process validation, worker training, and nonconformance handling. Price and reputation alone can mislead.
A changed furnace, cleaning chemical, or sub-tier source may affect implant quality. The clinical impact may not be obvious immediately.
No. Records show control, not perfection. One failed test or missing link deserves investigation before implantation.
Hold the affected lot, verify the result, review related records, and investigate possible mixed materials. We still miss things.
Raw material control in orthopedic implants covers the careful selection, inspection, testing, and documentation of metals, polymers, ceramics, and other materials used in implant production. Why is raw material control critical for orthopedic implants? Material purity and consistency directly influence strength, corrosion resistance, biocompatibility, fatigue life, and long-term patient safety. Even small variations or unwanted contaminants can affect manufacturing performance and increase the risk of implant failure.
Effective control begins with clearly defined material specifications and qualified suppliers. Each batch should be verified through chemical analysis, mechanical testing, dimensional inspection, and, when necessary, surface and microstructural evaluation. Complete traceability links raw materials to suppliers, test results, production records, and finished devices. These practices support reliable supplier qualification, consistent quality, and early detection of nonconformities. They also help manufacturers demonstrate compliance with applicable regulatory and quality requirements while reducing process variation and strengthening confidence in the safety, durability, and clinical performance of orthopedic implants.
 XOVEC Orthopedic Implants